At Apple Rubber, we understand the medical industry’s need for precision, dependability, and adherence to the highest of standards. When the success or failure of a life-saving medication, vaccine, medical material, or piece of equipment can depend on the effectiveness of a single sealing device, failure just isn’t an option.
We know that precision in medical sealing components is crucial for several reasons:
- Patient Safety: Ensures that medical devices function as intended, protecting patient well-being
- Device Reliability: Contributes to the longevity and consistent performance of medical equipment
- Contamination Prevention: Helps maintain sterile environments in critical medical applications
- Regulatory Compliance: Meets strict industry standards and regulations, full IQOQPQ documentation, and qualification for new part designs
Delivering high-quality medical rubber seals and providing excellent customer service and satisfaction are tenets at the core of everything we do at Apple Rubber.
How We Collaborate with the Medical Industry
Apple Rubber’s engineers are constantly working to offer top quality products, better testing, and more thorough documentation. The design engineers at Apple Rubber are always available to work directly with our medical industry customers.
We work with you through every step of the development process—from design and prototype to production and testing. It’s one of the many reasons our engineers are able to develop strong, reliable, medical-grade seals and devices that meet the high demands of critical medical environments.
About Our Products
All of the medical-grade elastomers at Apple Rubber are tested to FDA USP Class VI standards or ISO 10993 test protocols. These rigorous testing procedures ensure the safety and biocompatibility of the materials used in medical applications.
The elastomers we use feature improved chemical resistance, excellent heat resistance, low permeability to gas, and are compatible with different sterilization techniques. Our offerings include:
- Liquid Silicone Rubber (LSR) (-85°F to +400°F)
- Key benefits: Excellent biocompatibility and resistance to extreme temperatures
- Fluoroelastomer (FKM) (-13°F to +446°F)
- Key benefits: Outstanding chemical resistance and high-temperature performance
- Ethylene Propylene (EPDM) (-60°F to +275°F)
- Key benefits: Great resistance to steam, hot water, and polar solvents
In addition to our material offerings, Apple Rubber is proud to provide the following capabilities, all in-house at our US facility:
- 50 years of industry-specific engineering expertise
- Proficiency in polymer science and mold design
- 3D CAD and CAM technology in design and prototyping
- Assistance across every stage, from concept to seal validation
- Quality documentation spanning First Article to full IQOQPQ
- Sterilizable materials, such as ETO, Gamma, and Autoclave
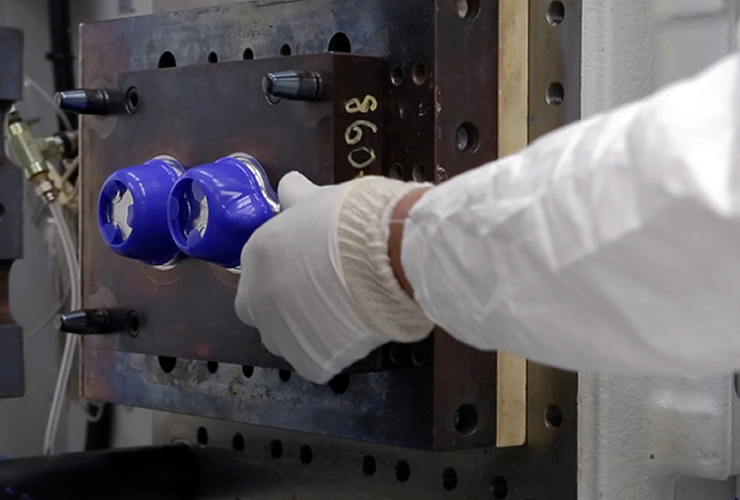
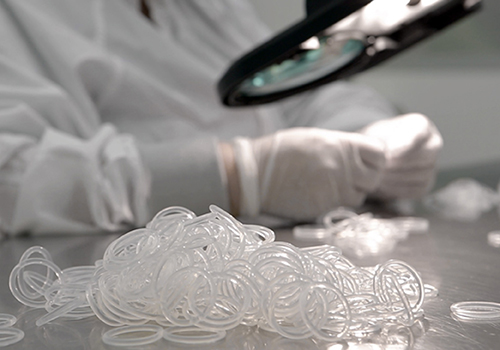
- Class 10000 ISO-07 cleanroom, LSR, and extensive medical-grade O-ring inventory
We continue to innovate in the field of medical rubber sealing by:
- Developing new, biocompatible materials
- Advancing microminiature sealing technologies
- Utilizing cold drop molds for low material scrap and flash extension
From simple seals to the most complex parts, Apple Rubber utilizes a host of sophisticated technologies and processes to consistently manufacture high-quality components. Our medical parts and seals are trusted by medical experts for use in countless pieces of life saving equipment, including:
- Ventilators
- Medical testing consumables
- Medical pump seals
- IV components
- Feeding devices
- Implant materials
Our Cleanroom Updates
We have expanded our cleanroom as our way of striving to be the leading sealing solution provider for the medical field where precision manufacturing, testing, and assembly are critical.
Highlights of our expansion include:
- Complete processing, including production, washing, and packaging area
- Four injection molding machines, mainly for liquid silicone rubber, and available for plastic or rubber
- Two post-cure ovens
- A Sprayflood washer system
- Fully automated ultrasonic parts cleaning system
The air handling system supplying our cleanroom has been tested under the requirements of
IEST RP CC0006.3 (Testing Cleanrooms) and has met ISO 14644-1:2015 (E) guidelines. As such, we have received a Certificate of Compliance from R. Kraft, Inc. This also means our cleanroom has met the following standards:
- The air handling system supplying the cleanroom area has been recently certified to ISO 14644-2 2000.09.15. (Testing and Monitoring), which corresponds to FS 209E Class 10000
- Air systems for the following areas have met ISO 14644-1 1999.05.10 guidelines to qualify for the following air cleanliness classifications:
- Main Cleanroom – ISO Class 7 (10000) in an “As-Built” mode of operation at .5 microns
- Inspection (Gown) Room – ISO Class 7 (10000) in an “As-Built” mode of operation at .5 microns
The Core of Everything
We deliver precision-molded custom sealing solutions at the core of today’s most advanced medical devices. Our o-rings, MicroSeals, and molded seals provide proven reliability for critical healthcare applications.
For more information on our medical parts and seals, contact the engineers at Apple Rubber.
Sponsored content by Apple Rubber Products